What Is the Best Industrial EMC Solution in 2026?
What Is the Best Industrial EMC Solution in 2026? The answer depends on the equipment, installation, and operating environment. A variable-frequency drive beside a long motor cable creates different electromagnetic challenges than a sensor cabinet near welding equipment. One product cannot solve every problem. Details matter.
EMC engineer and author Henry W. Ott is often credited with this practical advice: “The best way to solve EMC problems is to prevent them from occurring in the first place.” That principle shapes a reliable Industrial EMC Solution: address interference risks during design, not only after a failed test. Engineers may review cable routing, enclosure seams, bonding, filtering, and circuit-board layouts before choosing protective components. A ferrite or filter can help, but neither compensates for every poor installation choice.
This introduction examines how to compare solutions in 2026, from shielding materials and power-line filters to grounding practices and verification testing. It also considers conducted emissions, radiated emissions, and immunity under realistic operating conditions. Test results matter. So does the setup. A clean laboratory result may not reflect a dusty factory floor, a long cable run, or equipment switching under load. There is no perfect checklist, and some recommendations need revisiting when the site changes. The goal is not to promise zero interference. It is to select, install, and validate measures that fit the actual system—and to be honest about what remains uncertain.
Industrial EMC and Its Role in Reliable Equipment Operation
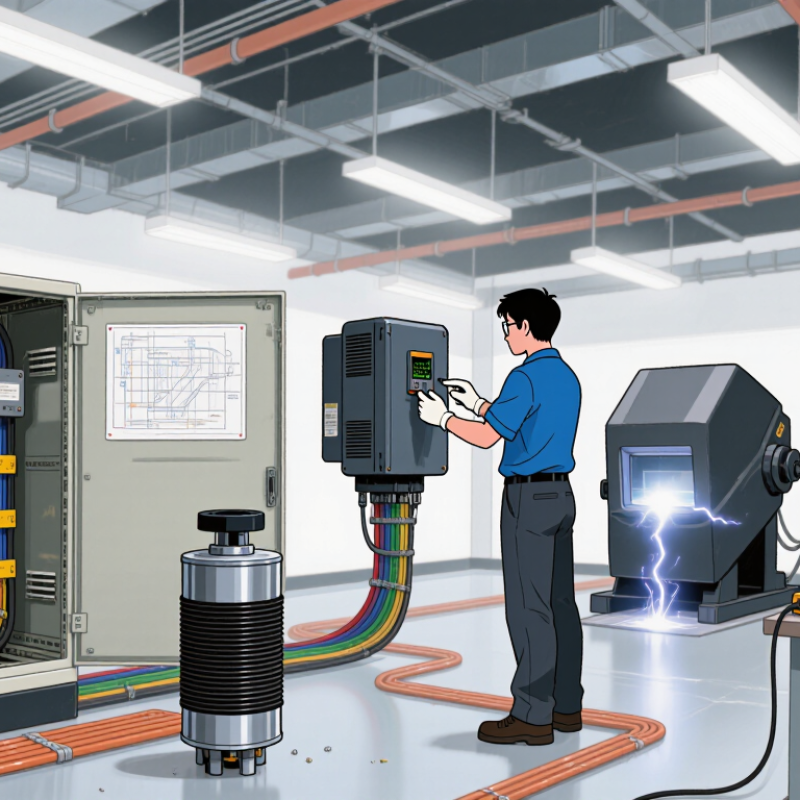
Industrial electromagnetic compatibility (EMC) helps equipment operate reliably amid electrical noise. In a factory, a variable-speed drive can disturb nearby sensor signals, while long cable runs may collect interference. The result may be a false reading, a reset, or an unexplained pause. Small disruptions matter. EMC is not only about passing a test; it is about keeping control and communication stable under real operating conditions.
A practical solution starts with the installation. Engineers should identify noise sources, sensitive circuits, cable routes, grounding points, and enclosure openings. Shielded cables, suitable filters, bonding, and physical separation can reduce interference when chosen for the actual system. Testing should include demanding operating states, such as motor starts and switching loads. Record cable lengths, grounding methods, and test conditions to make troubleshooting more repeatable. Still, no single measure fixes every site. A cabinet door, spare cable, or maintenance change can alter the path. That deserves attention.
Tips: Check sensor readings during motor start-up. Keep power and signal cables apart where practical. Verify shield termination against the design, not habit. Retest after modifications. Tiny changes count.
Industrial EMC and Reliable Equipment Operation
IEC 61000-4-2 contact-discharge test levels
The chart shows the four contact-discharge severity levels specified by IEC 61000-4-2: 2, 4, 6, and 8 kV. Testing equipment against the applicable immunity requirements helps assess its resistance to electrostatic discharge. The required level depends on the product standard and intended operating environment.
Source: IEC 61000-4-2, Electrostatic discharge immunity test.
Sources of Electromagnetic Interference in Industrial Environments
What Is the Best Industrial EMC Solution in 2026?
Sources of Electromagnetic Interference in Industrial Environments
Industrial interference often starts at ordinary equipment: variable-speed drives, switching power supplies, contactors, welders, and induction heaters. Fast switching can send noise along power and signal cables. Motors and long cable runs can also radiate energy into nearby sensors. A fault may appear only when a machine starts, a cabinet door closes, or a cable is moved. That timing is evidence.
The coupling path matters as much as the source. Conducted noise travels through shared supplies and grounding connections; radiated fields can affect unshielded cables or poorly bonded enclosures. IEC 61000-4-6 specifies conducted RF immunity testing from 150 kHz to 80 MHz. IEC 61000-4-3 covers radiated RF immunity from 80 MHz to 6 GHz and includes test levels such as 10 V/m. These ranges help engineers plan tests, but they do not identify every site-specific problem.
A useful investigation records the equipment state, cable routes, and disturbance timing before changing components. Then measure near suspected drives and cables, and compare results with the applicable IEC test methods. A spectrum analyzer can reveal narrow peaks; a current probe can help trace noise on a cable. The map will be imperfect. Production changes, and one overlooked cable can undo a careful fix.
Core Components of an Effective EMC Solution
What Is the Best Industrial EMC Solution in 2026?
Core Components of an Effective EMC Solution
An effective industrial EMC solution combines enclosure design, bonding, filtering, and disciplined cable routing. It is a system. A conductive enclosure can reduce radiated interference, but only when doors, seams, and access panels maintain reliable electrical contact. Small gaps matter. Keep painted surfaces away from bonding points, and use short, wide connections between panels and the protective bonding network. Long wires can add unwanted inductance, especially at higher frequencies. Check joints after maintenance, too; a design that works when new may change after repeated opening.
Filters should sit close to where power or signal cables enter the enclosure. Separate noisy motor cables from sensitive sensor wiring, and avoid bundling them together for convenience. On circuit boards, keep high-speed return paths continuous and minimize loop areas. Then test the complete machine under realistic operating conditions, including switching loads and long cable runs. Record the configuration and test results. No checklist catches every machine-specific coupling path, and a clean lab result may not reflect a busy factory floor. That gap deserves attention. Recheck after major wiring or equipment changes.
Selecting an EMC Approach for 2026 Industrial Requirements
Selecting an EMC approach for 2026 starts with the equipment’s real operating environment, not a generic filter package. A variable-speed drive beside a sensor cable creates a different risk from a radio transmitter near a control cabinet. The International Energy Agency’s Energy Efficiency 2023 report estimates that industry accounts for about 37% of global final energy use. More electrified processes mean more switching equipment and more opportunities for interference. Measure first.
Map likely noise sources, cable routes, enclosure openings, and sensitive inputs before changing hardware. IEC 61000-4-3 specifies radiated RF immunity test methods and levels; select an appropriate level for the product and its intended environment. In practice, test a running machine, not only an empty cabinet. Record sensor readings while motors start, drives ramp, and relays switch. That matters.
Then match controls to the failure path: improve bonding and shielding, separate noisy and signal cables, or add suitable filtering at the source. Verify each change with repeatable measurements and documented test conditions. A clean laboratory result can still mislead if the field wiring differs. I would treat that as a real limitation, not a footnote. Keep spare test points and accessible cable entries in the design, so troubleshooting does not require dismantling the whole panel.
Testing and Verifying EMC Performance in the Field
What Is the Best Industrial EMC Solution in 2026?
Testing and Verifying EMC Performance in the Field
A dependable industrial EMC solution must work beside real machinery, not only inside a test chamber. Field checks can reveal interference from variable-speed drives, long cable runs, and cabinet seams. IEC 61000-4-3 specifies radiated RF immunity test levels including 1, 3, and 10 V/m. IEC 61000-4-6 defines conducted RF testing. These standardized levels help set controlled benchmarks; they are not automatic guarantees of field performance.
Measure with calibrated equipment, and record antenna position, cable routing, machine load, and nearby equipment states. Repeat readings while motors start, slow down, and operate under load. Small details matter. A spectrum trace without operating notes can hide the cause of a disturbance. CISPR 16-1-1 sets requirements for measuring equipment used in emissions testing, supporting consistent, comparable results.
Field conditions are rarely tidy. Reflections from metal surfaces can shift readings, while a temporarily quiet production line may conceal an intermittent problem. Compare results with a controlled baseline, then investigate repeatable peaks at the actual cable or enclosure involved. It takes time. A practical verification record should include instrument calibration status, measurement uncertainty, test location, and corrective changes. Even then, one site visit may not capture every operating condition, so schedule checks during representative production cycles.